
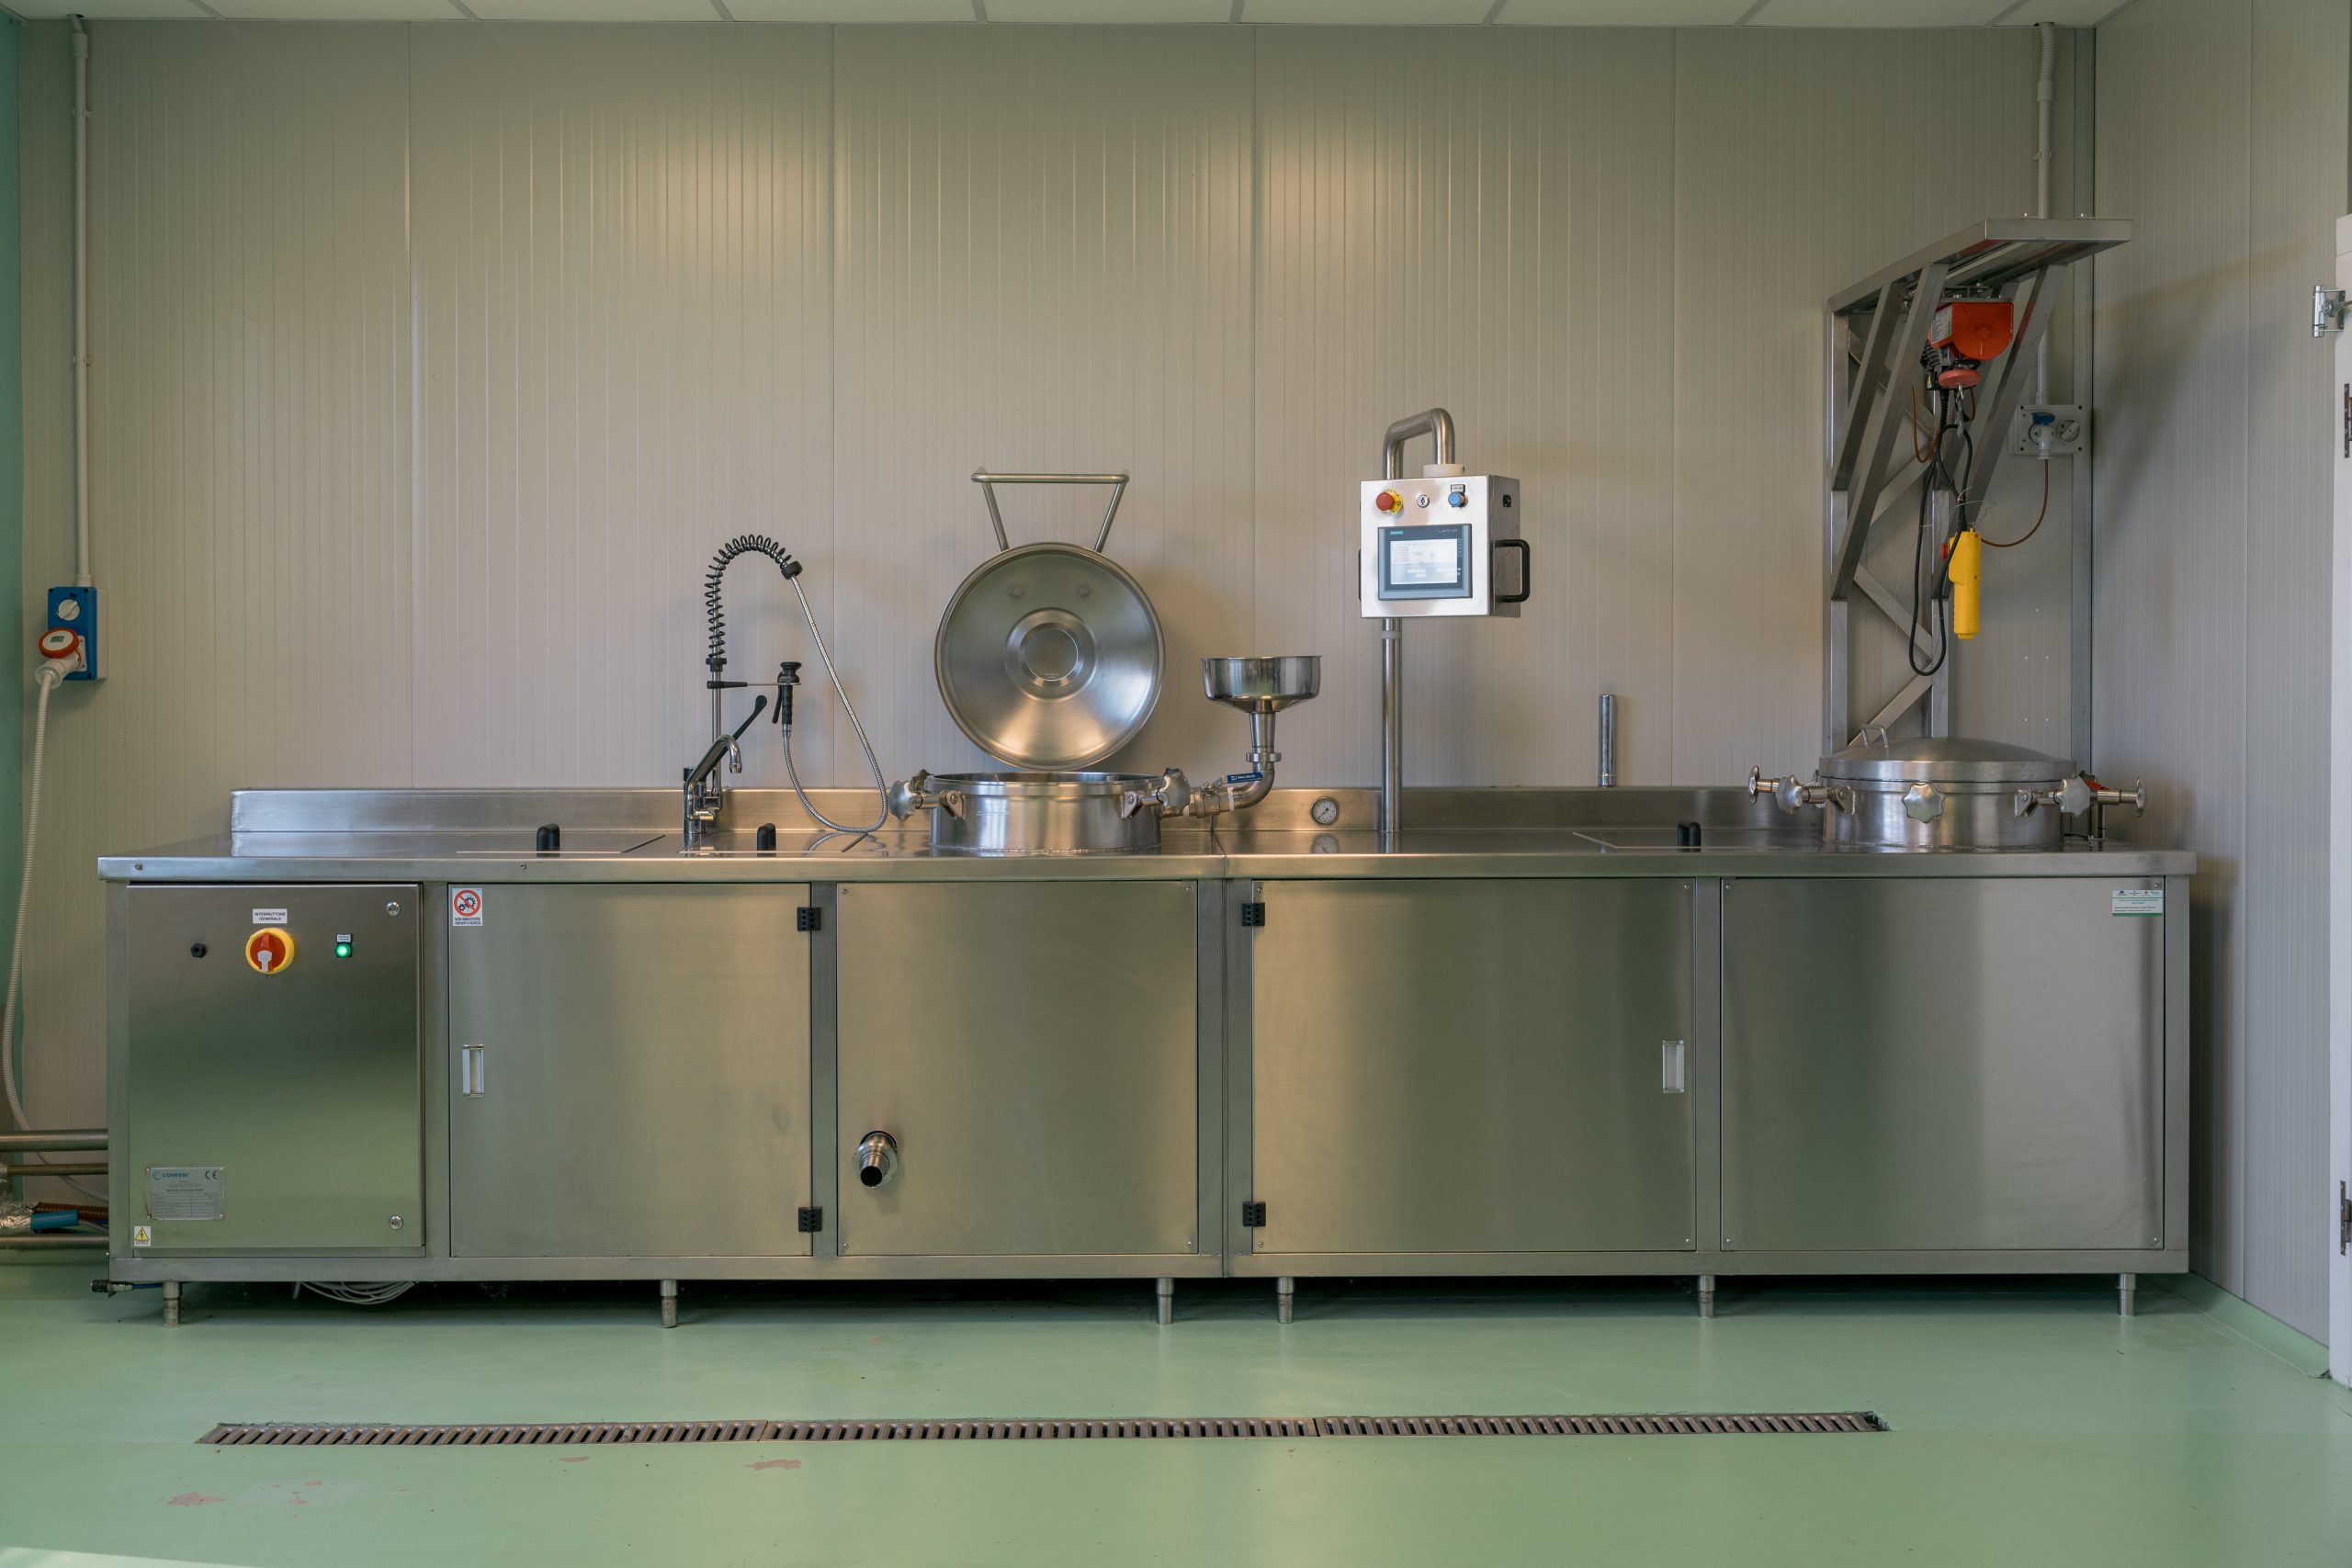
In the landscape of small agri-food businesses, the Multipurpose Workstation stands out as the ideal solution for food processing.
The Multipurpose Workstation is a professional system that allows a single machine to produce jams, preserves, juices, sauces, creams, and other foods, through controlled, standardized, repeatable, and configurable processes tailored to the customer’s production needs. For those working with candied fruit, the unit also handles this process within the same plant, without requiring a dedicated machine.
The main mistake made by those starting a food lab is thinking they can manage the entire production with domestic-type equipment. Alternatively, those who transform raw materials into ready-to-consume products — jams, sauces, juices, preserves, candied fruit, pickles — often rely on numerous costly machines, disconnected from one another, low-tech, and complex to coordinate. In both cases, production processes end up slow, product standardization is not guaranteed, labor requirements are high, and production struggles to grow.
The Multipurpose Workstation was created precisely to overcome these issues, bringing together all processing stages in a single, automated and traceable plant.
What is the Multipurpose Workstation ?
The Multipurpose Workstation is a compact and versatile machine, made of stainless steel and designed for labs, small industries, and R&D departments. Within a single plant, it manages the washing, cooking, concentration, pasteurization/sterilization, candying, and — depending on configuration — packaging stages.
It is built around one or more independent tanks, available in different sizes based on the customer’s production needs, heated via a thermal liquid jacket on the walls and bottom. Scraper blades keep the product in constant motion, preventing it from sticking or burning locally.
Each stage is managed via a 10-inch touchscreen, which allows the operator to set temperature, process time, °Brix level, and pasteurization curve just once, save them as a recipe, and recall them for every production run — eliminating the variability tied to individual operator sensitivity.
Thanks to integration with Industry 4.0 systems, the multifunction unit enables remote monitoring, software updates, and data logging for every cycle, exportable via USB — a requirement increasingly demanded by food regulations and by foreign markets with strict documentation controls.
The processing stages and their respective benefits for the product using the Coveser Multipurpose Workstation
- Vacuum cooking. Processing under vacuum lowers the product’s boiling temperature, making it possible to carry out cooking and concentration at lower temperatures than traditional processes. This preserves color, aroma, vitamins, and heat-sensitive compounds that prolonged high-temperature cooking would otherwise degrade — a decisive advantage for fruit, vegetables, and any heat-sensitive raw material. The result is superior quality and stability of the finished product, with more uniform consistency and optimized shelf life.
- Vacuum concentration. Using the same principle, the multifunction unit reduces the water content of the product until the desired density is reached, without needing to extend cooking times. A process particularly useful for jams, preserves, concentrated juices, and high-density sauces.
- Pasteurization and sterilization. The thermal cycle applied to the jar or packaged container reaches 121°C, thanks to built-in algorithms, or through manually set parameters based on the product’s pH. The choice between pasteurization and sterilization depends on the type of product and the desired shelf life.
Productivity benefits of the Multipurpose Workstation.
- Adopting a single system instead of several separate machines saves space, reduces energy consumption, lowers maintenance interventions, and reduces the probability of error.
- The same machine also allows different products to be made, easily switching from preparing a vegetable preserve to a jam, or from a cream to a tomato sauce.
- Independent double tanks allow two batches to be managed in parallel — for example, two different recipes, or cooking and pasteurization at the same time — increasing production capacity without additional machines.
- Versatile heating: available in steam or electric versions, to adapt to the energy resources already available on-site and reduce operating costs.
- Built-in traceability, which simplifies compliance with food regulations and inspection management, including in foreign markets.
- Batch-to-batch standardization, thanks to recipes saved in the system, which also reduce training time for new operators, since every batch follows repeatable parameters.
What products can you process with the Coveser Multipurpose Workstation
The Multipurpose Workstation is designed for a wide range of food transformations. Main processes:
- Jams and preserves Vacuum cooking and concentration preserve the fruit’s color and aroma, with pasteurization parameters calibrated to the product’s pH to ensure shelf life and food safety. Learn more in Multipurpose Workstation for Jams and Preserves.
- Ready-made sauces Uniform cooking and density control ensure consistent texture and flavor stability over time, batch after batch. Learn more in [link to ready-made sauces article].
- Fruit juices Vacuum concentration reduces the product’s water content while preserving its natural nutrients, without resorting to high temperatures that would compromise flavor and nutritional value.
- Vegetable preserves Optimized thermal treatments ensure the food safety required for this type of processing, while maintaining the texture and flavor of the vegetables.
- Candied fruit The candying process, managed within the same plant, ensures precise control over the sweetness and aromatic balance of the finished product.
Why choose the Coveser Multipurpose Workstation
If production varies throughout the year, the Multipurpose Workstation proves to be the most effective answer: a single plant capable of adapting to different processes, without changing the production workflow or having to invest in additional machines.
The Coveser Multipurpose Workstation brings together vacuum cooking, concentration, candying, and sterilization/pasteurization in a single machine. A solution designed for those who want to grow in volume without sacrificing the artisanal quality of the product.
What production capacity does the Multipurpose Workstation have?
The Coveser multifunction unit is available in different models depending on customer needs. It features either a single tank or independent double tanks. The two tanks can work in parallel — for example, two different recipes, or two different stages of the same product — increasing output without the need for additional machines.
What heating options are available?
The machine is available in steam or electric versions, allowing it to adapt to the energy resources already available on-site and optimize operating costs.
Is the Multipurpose Workstation suitable for small labs, or only for industrial production?
It is designed for a wide range of settings: artisanal labs, small food industries, and R&D departments. The ability to save recipes and recall them for every production run makes it suitable even for businesses without a dedicated technical team, since it eliminates the variability tied to individual operator sensitivity.
How much does a Coveser Multipurpose Workstation cost?
The price varies depending on the configuration (tank capacity, heating type, requested options). For a customized quote based on your production volumes, you can request a quote directly from the product page or contact the Coveser team for a free consultation.
Request a free consultation
To find out which configuration best suits your volumes and products.
